Precision Thread Grinding Services in the UK: Metrological Rigor and Supply Chain Integration
An in-depth analysis of high-precision thread grinding technology, metallurgical tolerances, and local OEM compliance frameworks for British advanced engineering hubs.
The United Kingdom’s advanced manufacturing sector—spanning the Sheffield Advanced Manufacturing Innovation District, the West Midlands Aerospace Corridor, and Scotland’s energy clusters—demands unmatched geometrical accuracy in threaded components. High-precision thread grinding services represent the pinnacle of rotary abrasive machining, overriding the physical and dimensional limitations of single-point thread turning, thread chasing, or roll threading on pre-hardened alloys.
When engineering critical mechanical links such as orthopedic spinal screws, flight-control ballscrews, surgical robotic lead screws, or high-torque turbine clamping fasteners, conventional machining fails to maintain pitch diameter consistency under extreme mechanical shear. Thread grinding utilizes vitrified and Superabrasive Cubic Boron Nitride (CBN) or electroplated diamond wheels operating under continuous oil-cooled creep-feed parameters. This delivers sub-micron lead accuracy, eliminates micro-cracking, and achieves mirror-like surface roughness metrics ($Ra < 0.1\mu m$).
1. Kinematic Superiority of CNC Thread Grinding over Conventional Machining
In high-specification UK manufacturing, the choice of thread generation method directly governs assembly validation, dynamic backlash, and tribological wear. Standard single-point cutting leads to tool deflection when machining materials above 45 HRC (such as heat-treated 17-4PH, Inconel 718, or Custom 465 stainless steel). Thread grinding solves this through high-rigidity synchronized multi-axis CNC wheel head kinematics.
| Metrological Parameter | CNC Thread Grinding | Single-Point CNC Turning | Cold Roll Threading |
|---|---|---|---|
| Pitch Diameter Tolerance | ±0.001 mm (±1μm) | ±0.012 mm | ±0.025 mm |
| Lead Accuracy (per 300mm) | ≤ 0.002 mm (Class 1) | ≤ 0.015 mm | ≤ 0.030 mm |
| Surface Roughness ($Ra$) | 0.05 μm – 0.2 μm | 0.8 μm – 1.6 μm | 0.4 μm – 0.8 μm |
| Workpiece Hardness Capability | Up to 68 HRC (Post-Heat Treatment) | Limited (≤ 45 HRC) | Ductile metals only (≤ 36 HRC) |
| Thread Profile Flexibility | Unlimited (Micro, Bone, ACME, Custom) | Standard ISO/UN profiles | Fixed roll die geometries |
| Root Radius Integrity | Continuous optical wheel dressing | Tool wear causes radius drift | Material flow overlaps |
UK Precision Industries Utilizing Advanced Thread Grinding Services
UK OEMs operate under rigorous quality systems backed by BSI, UKCA marking, and NHS procurement mandates. Our high-precision contract thread grinding capability integrates seamlessly into major UK industrial sectors:
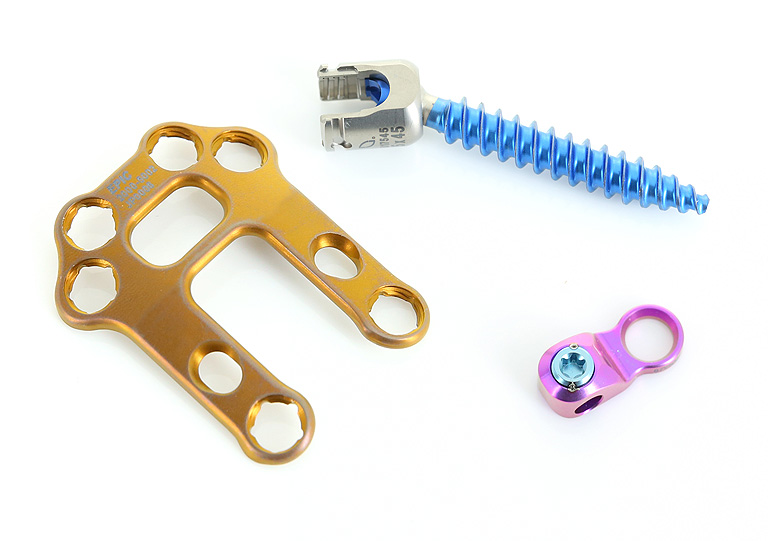
- Medical Devices & Orthopedics: Cannulated pedicle screws, spinal fixation rods, bone plates, and dental implant abutments requiring ISO 13485 validated passivated surfaces.
- Aerospace & Defense Tier-1 Suppliers: AS9100-compliant actuation screws, landing gear thread shafts, engine housing studs, and missile guidance fins.
- Surgical Robotics & Automation: Zero-backlash planetary miniature lead screws engineered for robotic end-effectors and automated laboratory testing gear.
Orthopedic & Spinal Threading
Grinding asymmetric buttress, dual-lead, and variable-pitch threads directly into biocompatible titanium ELI and PEEK polymers for NHS orthopedics suppliers.
Micro-Thread Dental Grinding
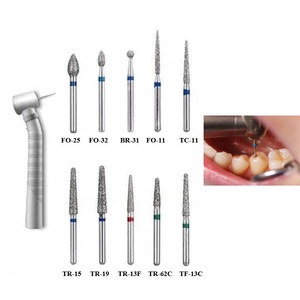
Ultra-fine thread forms down to M0.6 pitch for dental implants, internal locking taper screws, and high-speed handpiece FG burs under sterile cleanroom controls.
Precision Tooling & Cutters
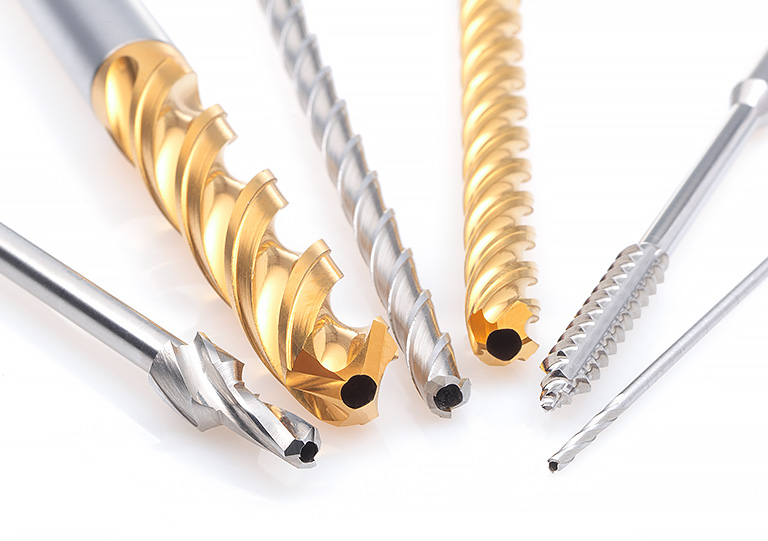
Thread grinding taps, reamers, end mills, and custom high-speed steel (HSS-Co) cutting tools engineered for the UK automotive and die-making industry.
Aerospace Actuation Shafts
Internal and external thread grinding on high-strength alloys (Inconel 718, Waspaloy, Titanium Grade 5) adhering to defense supply chain requirements.
Robotics & Stepper Motor Drives
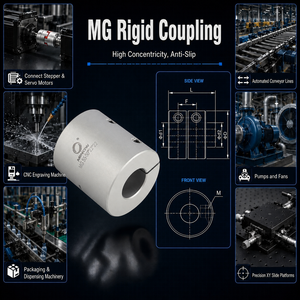
Sub-micron pitch accuracy clamping screws, shaft couplers, and anti-backlash lead screws utilized in automated 3D printing and laser processing lines.
Subsea & Energy Actuators
Heavy-duty ACME and Trapezoidal thread grinding on corrosion-resistant duplex stainless steel for North Sea energy flow-control valves.
Localized Strategic Trends Reshaping UK Precision Thread Manufacturing
How British OEMs are adapting to post-Brexit compliance, Net-Zero carbon targets, and hybrid Additive-Subtractive manufacturing workflows.
The UK precision engineering landscape is experiencing a structural migration toward smart, low-carbon, and highly validated manufacturing processes. Driven by the UK Government’s High Value Manufacturing Catapult framework and evolving healthcare directives, contract thread grinding suppliers must deliver technical advantages beyond standard machining capabilities.
1. Convergence of Additive Manufacturing (PBF) and Precision Thread Grinding
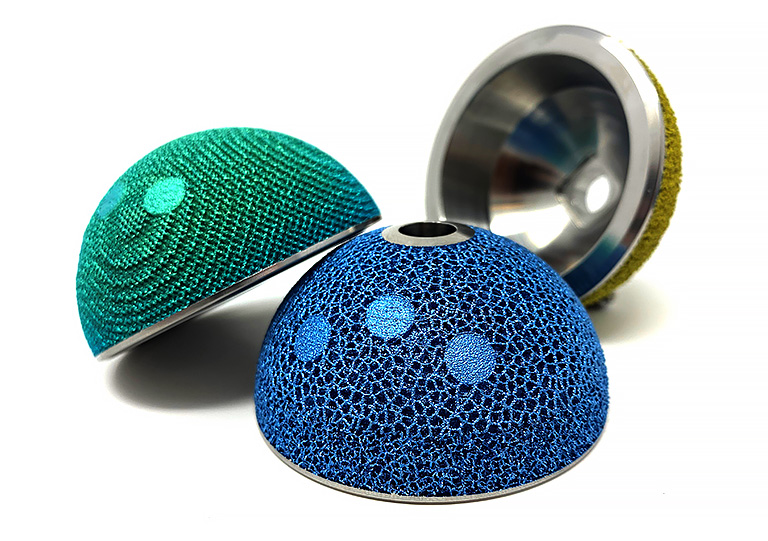
With the UK leading early adoption of Powder-Bed Fusion (PBF) 3D printing for orthopedic implants and aerospace brackets, unmachined additive surfaces exhibit rough textures ($Ra > 10\mu m$) unsuitable for load-bearing thread interfaces. Modern UK OEMs utilize hybrid workflows: additive printing of complex lattice bone-ingrowth structures followed by secondary 5-axis CNC thread grinding to establish micron-accurate thread roots without inducing thermal distortion.
2. UKCA Regulatory Compliance and ISO 13485:2016 Traceability
Following the UK Medical Devices Regulations, medical device OEMs supplying the NHS require complete lot traceability, Material Test Reports (MTRs), and full Device Master Record (DMR) documentation. Quality assurance protocols must incorporate automated Coordinate Measuring Machine (CMM) touch probing and non-contact optical laser scanning for 100% thread profile verification.
Why Leading UK OEMs Partner with Our Precision Manufacturing Network
FDA-registered, ISO 13485-certified single-source contract manufacturing for implants, surgical instruments, and robotics assemblies.
Certified & Audit-Ready
FDA-registered operations certified to ISO 13485 standard. Complete compliance documentation, first-article inspection (FAI), and full raw material lot traceability for regulatory dossier submission.
End-to-End Contract Support
Eliminate multi-vendor handoff risks. We integrate engineering design-assist, CNC Swiss turning, thread grinding, cleanroom passivation, electropolishing, and modular assembly under one quality management system.
Micron-Level Metrology
In-process laser gauging and optical profile dressed grinding wheels ensure continuous pitch diameter, flank angle, and thread depth consistency across prototype to high-volume production batches.
MedTorque Surgical Tools Integration
Proprietary capabilities in custom silicone-handled instruments, fixed, ratcheting, and torque-limiting couplings designed for orthopedic and spinal surgical trays.
Advanced Metallurgical Expertise
Decades of specialized grinding experience across medical-grade stainless steel (316L, 17-4PH, 440C), Titanium grade 5, Cobalt-Chrome alloys, PEEK, and nitronic aerospace steels.
Rapid UK & Global Logistics
Streamlined supply chain integration, flexible stocking agreements, and fast turnaround prototyping for British engineering teams requiring short lead times.
UK OEM Procurement & Technical FAQ
Clear answers to common technical, regulatory, and commercial inquiries from UK procurement managers and engineering teams.
What thread profile tolerances can your grinding services achieve?
Our high-precision CNC thread grinding machinery consistently holds pitch diameter tolerances to ±0.001 mm (±1 micron) and lead error within ≤ 0.002 mm per 300 mm length. Surface finishes down to Ra 0.05 μm are routinely maintained on hardened titanium, stainless steels, and exotic cobalt-chrome alloys.
Are your facilities certified for UK medical device supply chains (ISO 13485)?
Yes. Our manufacturing infrastructure operates under an FDA-registered and ISO 13485:2016 certified Quality Management System. We fully support UKCA regulatory requirements, supplying Certificate of Conformity (CoC), raw material mill test reports, passivation reports, and FAI inspection data suitable for inclusion in your Device Master File (DMF).
Can you grind internal threads as well as external threads on sub-miniature medical components?
Absolute precision is guaranteed for both internal and external thread grinding. We specialize in micro-thread forms down to M0.6 for dental implants, surgical robotics components, and custom cannulated pedicle screws using high-speed internal grinding spindles and dressable diamond wheels.
How does thread grinding compare to thread milling for 3D printed additive implants?
Thread milling on additive parts often causes micro-burrs and tool chatter due to material density variations. Thread grinding provides a continuous abrasive cut that eliminates surface tear, removes brittle oxide layers, and introduces beneficial compressive residual stress, significantly raising fatigue strength for implants.
What is the standard lead time for shipping prototype or production runs to the UK?
Prototype samples and DFM feedback can typically be delivered within 5 to 10 working days via express logistics. Production batches are scheduled based on customer blanket orders or VMI stocking arrangements, ensuring seamless delivery directly to UK manufacturing sites in England, Scotland, Wales, or Northern Ireland.
How do we initiate a DFM review or request a quotation for thread grinding?
Simply click the "Contact Us" button anywhere on this page to open our direct communication portal, or submit your 3D CAD models (STEP/IGES) and 2D engineering drawings with thread callouts. Our senior application engineers will evaluate manufacturability and provide a comprehensive quotation within 24 hours.
Accelerate Your UK Precision Engineering Program
Partner with an FDA-registered, ISO 13485-certified thread grinding specialist. Get expert DFM analysis and precision quotation within 24 hours.