Precision Components & Surgical Testing Equipment
Engineered for exacting biomedical, diagnostic, and surgical applications, meeting rigorous UKCA, CE, and FDA regulatory standards.
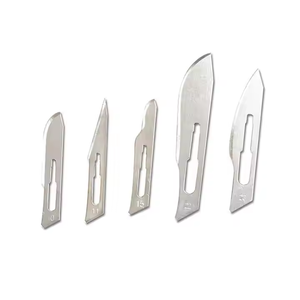
Super Quality Medical Stainless Steel Surgical Scalpel Blade Carbon Steel Surgical Blade With Different Sizes
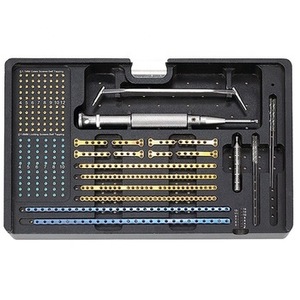
1.6mm Locking Plate Instrument Kit Small Animals Orthopedic Veterinary Surgical Instruments Drill Guide Implants Bone Plate
Medical Grade GR1 GR2 Titanium Wire ASTM F67 F136 0.15-8mm Biocompatible for Implant Surgical Applications OEM
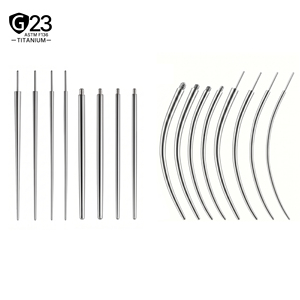
ASTM F136 Titanium Threadless Threaded Piercing Insertion Tapers 14G 16G 18G 20G Curved Needle Body Piercing Titan De Titanio
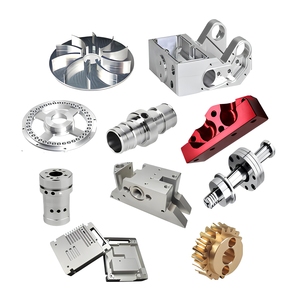
Cnc Machining Service Custom Cnc Parts CNC Turning Spare Parts Custom Medical Parts
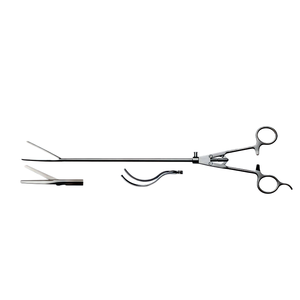
Minimally Invasive Manual Thoracic Clamp-High Quality 220MM Single-Jointed Reusable for Lung Grasping and Laparoscopic Surgery
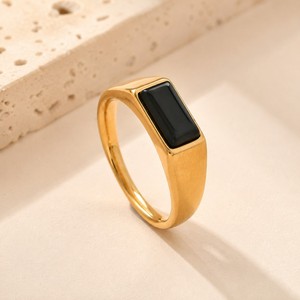
TouchLove Nickel Free Surgical Steel Stainless Steel Rings Cubic Zirconia Casual/Sporty Geometric Shape REACH Compliant EU US AU
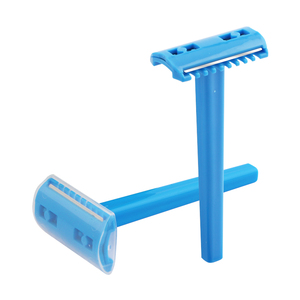
Disposable Surgical Prep Razor Double Edge Safety Razor Medical Use Stainless Steel Blades
High-Precision Manufacturing for Greater London's Bio-Cluster Ecosystem
An executive overview of OEM supply chain engineering, metallurgical compliance, and micro-component manufacturing for diagnostic, clinical, and laboratory equipment in the UK.
London's Life Sciences Hub & Procurement Realities
London has solidified its position as Europe’s premier life sciences innovation capital. Anchored by the UK Golden Triangle (London, Oxford, and Cambridge), districts such as the King’s Cross Knowledge Quarter, Imperial College’s White City Innovation District, and the Sutton London Cancer Hub host hundreds of advanced biotechnology firms, clinical research facilities, and medical diagnostic OEMs.
However, scaling next-generation life sciences testing equipment—from high-throughput DNA sequencers to automated in-vitro diagnostic (IVD) analyzers—requires mechanical components built to sub-micron tolerances. Sourcing teams in Greater London face mounting pressures regarding supply chain transparency, regulatory friction post-UKCA implementation, and stringent material biocompatibility.
Eliminating Supply Chain Vulnerabilities for UK OEMs
As a global contract manufacturer and specialized exporter, Greyack Medical bridges the gap between high-level bio-engineering designs and commercial-scale manufacturing. Operating under rigorous ISO 13485:2016 quality management systems and FDA establishment registration, we supply custom instrument components directly to London-based OEMs, research laboratories, and medical tech firms.
By combining multi-axis CNC Swiss turning, powder-bed fusion additive manufacturing, high-precision flute grinding, and validated passivation workflows, we deliver components that satisfy both UK MHRA requirements and international market standards without inflated lead times.
End-to-End Precision Manufacturing Disciplines
Four specialized manufacturing divisions consolidated under one rigorous quality system to guarantee mechanical accuracy and batch-to-batch repeatability.
Precision CNC Machining
State-of-the-art 5-axis CNC machining and high-speed Swiss lathe turning engineered specifically for micro-scale medical and bio-testing components.
- Sub-micron dimensional accuracy
- Complex fluidic manifolds & housings
- Swiss turning for fine pinions & shafts
Additive Manufacturing
Direct Metal Laser Sintering (DMLS) and powder-bed fusion additive processes that create highly complex bio-structures and micro-channel geometries.
- Titanium & Stainless Steel printing
- Integrated internal micro-channels
- Rapid DFM prototyping to scale
Medical Tool Grinding
High-precision flute grinding, thread grinding, and needle point forming using diamond-wheel CNC grinding centers for sharp surgical tools.
- Razor-sharp drill points & reamers
- Consistent burr-free edge retention
- Micro-instrumentation grinding
Finishing & Assembly
Validated citric and nitric acid passivation, electropolishing, laser etching, silicone-handle overmolding, and cleanroom class 7 sub-assembly.
- ASTM A967 compliant passivation
- MedTorque ergonomic handle assembly
- Laser marking & lot verification
Metallurgical Specifications for Life Sciences Applications
Selecting the optimal bio-compatible alloy or engineered polymer is critical to preventing galvanic corrosion, leaching, and mechanical failure in diagnostic testing environments.
| Material Designation | Applicable Standards | Key Mechanical Properties | Biocompatibility & Compliance | Typical Testing Equipment Applications |
|---|---|---|---|---|
| Titanium Grade 5 (Ti-6Al-4V ELI) | ASTM F136 / ISO 5832-3 | High strength-to-weight ratio, extreme fatigue resistance, non-magnetic | ISO 10993 compliant, exceptional tissue & fluid inertness | Centrifuge rotors, microfluidic manifold blocks, surgical robotic effectors |
| Titanium Grade 1 & 2 (CP Ti) | ASTM F67 / ISO 5832-2 | Unalloyed pure titanium, superior ductility, maximum corrosion resistance | High bio-inertness, resistant to aggressive laboratory reagents | Reagent dosing pins, implantable sensors, analytical probe sleeves |
| Medical Grade Stainless Steel 316L | ASTM A276 / ISO 5832-1 | High corrosion resistance, low carbon content preventing carbide precipitation | REACH & EU MDR compliant, passivated per ASTM A967 | Spectrometry fluid lines, scalpel blades, diagnostic housings, razors |
| Martensitic Stainless Steel (420 / 630 / 17-4PH) | ASTM F899 | High hardness upon heat treatment, wear resistance, edge retention | Standard clinical instrument compliance, chemical passivation ready | Surgical clamps, cutters, bone plates, high-torque drive couplings |
| PEEK (Polyetheretherketone) Medical Grade | ASTM F2026 | Radiolucent, high chemical resistance, autoclavable without degradation | USP Class VI certified, non-conductive bio-polymer | Insulated surgical handles, micro-dispensing valves, HPLC fittings |
Localized Application Scenarios across Greater London
Providing custom-engineered component solutions tailored to specific life sciences and clinical sectors operating within London’s advanced innovation zones.
1. Microfluidics & In-Vitro Diagnostics (IVD) Analyzers
London’s leading diagnostic start-ups and genomics laboratories demand micro-machined manifold components with zero internal burrs. Greyack Medical manufactures custom titanium (ASTM F67/F136) dosing needles, micro-valve bodies, and optical fluidic blocks holding internal diameter tolerances down to ±0.002 mm. These components withstand aggressive bio-reagents and continuous automated thermal cycling without degradation.
2. Surgical Robotics & End Effectors
Working alongside cutting-edge robotic surgical developers affiliated with London’s major NHS teaching trusts, we deliver lightweight, high-torque components. Utilizing multi-axis CNC Swiss precision turning, we produce miniature drive gears, silicone-handled ratcheting couplings, and titanium micro-articulation joints designed for minimally invasive robotic arms and laparoscopic tooling.
3. Automated Bio-Sample Storage & Centrifugation
High-throughput automated biobanks and cell-therapy processing centers rely on mechanical components capable of enduring cryogenic temperatures and violent rotational forces. We export high-precision balanced centrifuge rotors, titanium tube racks, and automated gripper assemblies crafted from medical-grade 17-4PH stainless steel and PEEK to eliminate metal-flake contamination.
4. Optical Spectrometry & Liquid Chromatography (HPLC)
For life sciences testing equipment manufacturers producing high-performance liquid chromatography (HPLC) instruments, component surface finish is paramount. Our diamond-burnished surface finishes (Ra < 0.1 µm) and passivated 316L stainless steel capillary tubes prevent sample absorption, ensuring absolute measurement fidelity for chemical analysis.
Macro Trends Shaping UK Life Sciences Component Sourcing
Key regulatory changes, technological shifts, and supply chain strategies influencing procurement decision-makers in the UK market.
1. UKCA Certification Transition & MHRA Alignment
Post-Brexit regulatory frameworks necessitate strict compliance with both UKCA marking and ongoing EU MDR / IVDR directives. OEM procurement teams in London must ensure overseas suppliers deliver comprehensive technical documentation packages. Greyack Medical provides full raw material test reports, certificates of conformance (CoC), and dimensional inspection sheets to facilitate seamless MHRA technical file filings.
2. Demand for Near-Zero Lead Time Prototyping
With massive venture capital inflows into London biotech startups, time-to-market is the ultimate competitive advantage. Companies can no longer afford 16-week lead times for custom test rig components. By leveraging hybrid additive manufacturing and high-speed CNC turning, we supply validated DFM prototypes in days, accelerating regulatory submission timelines.
3. ESG & Sustainable Medical Supply Chains
NHS Net Zero mandates and corporate ESG standards have pushed UK device manufacturers to audit their supply chains for environmental impact and material waste. Our precision powder-bed fusion additive processes reduce scrap metal waste by up to 70% compared to traditional subtractive machining, aligning directly with London firms' sustainability targets.
The Greyack Manufacturing Advantage
Enterprise credentials, rigorous quality assurance, and global export infrastructure designed to satisfy the world's most demanding medical OEMs.
FDA Registered & ISO 13485 Certified
Our operations adhere strictly to international medical device quality standard ISO 13485:2016. Every batch undergo formal first article inspections (FAI) and process validation (IQ/OQ/PQ).
Proprietary MedTorque Engineering
We manufacture specialty MedTorque ergonomic silicone handles, ratcheting mechanisms, and torque-limiting couplings that deliver surgeon-grade tactile feedback and long-term durability.
Micro-to-Massive Precision Scaling
Whether you require micron-scale titanium piercing pins, complex 1.6mm orthopedic locking plate kits, or large-scale structural equipment housings, our facilities scale seamlessly from low-volume prototypes to high-volume production.
Streamlined Logistics to London & UK Hubs
With established export pathways, customs clearance handling, and dedicated account support, we provide reliable, duty-compliant door-to-door delivery across Greater London and the UK Golden Triangle.
London Life Sciences Procurement FAQ
Detailed technical and regulatory answers for engineering leads and procurement managers qualifying overseas suppliers.
Is Greyack Medical ISO 13485 certified and registered for exports to the UK?
Yes. Greyack Medical maintains an FDA-registered establishment and is fully certified under ISO 13485:2016 for medical device contract manufacturing. We regularly export precision componentry to life sciences OEMs, diagnostic laboratories, and medical device innovators throughout London and the broader UK market. Full certification packages are provided during supplier qualification audits.
What technical quality documentation is provided with component shipments to London?
Every shipment includes a comprehensive quality dossier: Material Test Reports (MTRs) detailing chemical composition and mechanical properties, Certificate of Conformance (CoC), CMM Dimensional Inspection Data, Passivation Verification (per ASTM A967/A380), and complete lot traceability numbers to support your Device History Record (DHR) and UKCA/MHRA compliance files.
Can you manufacture micro-fluidic manifolds and testing components in Titanium Grade 5 and PEEK?
Absolutely. We specialize in machining challenging bio-compatible materials including Titanium Grade 5 (Ti-6Al-4V ELI per ASTM F136), Grade 1/2 Pure Titanium (ASTM F67), Medical Grade Stainless Steels (316L, 17-4PH, 420), and engineered polymers such as PEEK (ASTM F2026). Our multi-axis CNC machines hold micro-fluidic tolerances down to ±0.001 mm with surface finishes as fine as Ra 0.1 µm.
How do you support Design for Manufacturability (DFM) during the prototyping phase?
Our senior application engineers review your 3D CAD files (STEP/IGES) and technical drawings early in the design cycle. We analyze wall thicknesses, deep-hole drilling ratios, tool clearance, and material stress profiles to recommend cost-saving DFM optimizations before production starts, reducing overall unit cost and preventing manufacturing delays.
What is the typical turnaround lead time for custom component orders exported to the UK?
For prototype samples and early-stage evaluation batches, our standard turnaround is between 5 to 10 working days depending on complexity and surface finishing requirements. Full-scale production runs typically ship within 3 to 4 weeks via air express directly to your facility in Greater London, complete with expedited UK customs clearance support.
Partner with a World-Class OEM Component Manufacturer
Accelerate your life sciences testing equipment development with precision micro-machining, certified biocompatible materials, and dedicated technical support for the London market.