High-Precision Flute Ground End Mills & Grinding Solutions
Direct factory supply of solid carbide end mills, roughing flutes, tungsten carbide rotary burrs, and superabrasive CBN grinding wheels engineered for heavy industrial tooling in Southern Vietnam.
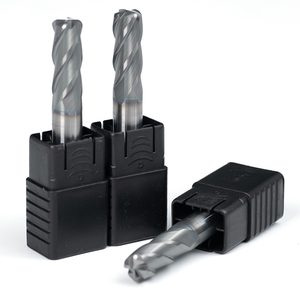
Factory Direct 4-Flute Corner Radius End Mill High-Precision Mold-Specific Solutions
Engineered with custom flute rake angles for die & mold steel grinding applications in high-speed machining centers.
Send an Inquiry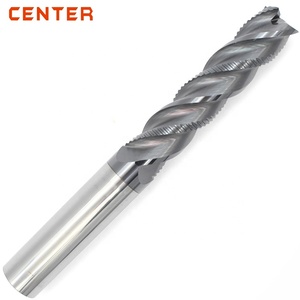
CENTER 4 Flute Roughing End Mill
Designed with wave-shaped chipbreaker flutes to maximize material removal rates in alloy steel and titanium roughing operations.
Send an Inquiry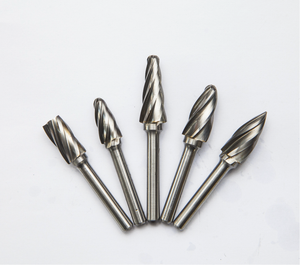
Carbide AlTin Coated 4 Flutes Face Mill Double Diamond Cut CNC Router Tool
Features ultra-dense AlTiN PVD coating and precision diamond-ground flutes for superior wear resistance during continuous milling.
Send an Inquiry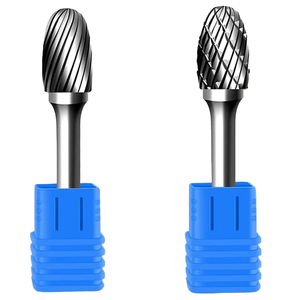
OEM Supported Single-Cut/Double-Cut Cylindrical Shank Tungsten Carbide Rotary Burrs
Master-ground helical flutes provide clean deburring, edge blending, and rapid stock removal across hard metal fabrications.
Send an Inquiry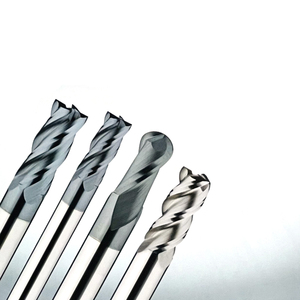
Precision End Mills Helical Flute Cutting Tools with Cylindrical Shank
Sub-micron carbide substrate with mirror-polished flute surfaces ensuring frictionless chip evacuation in general industrial milling.
Send an Inquiry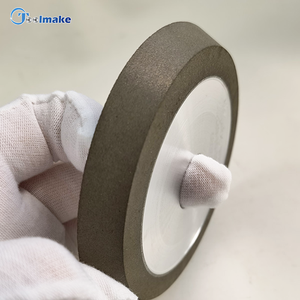
Precise 1V1 Type CBN Grinding Wheels for Flute and End Mill Processing
Designed for multi-axis CNC grinding machines (ANCA, Walter) to fabricate micro and macro tool flutes at high RPM speeds.
Send an Inquiry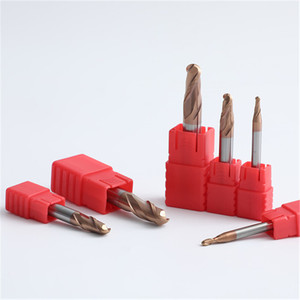
Wholesale High Quality Ball Endmill Grinder 2 Flute Carbide End Mill
Optimized 2-flute ball nose geometric relief angles designed for 3D contour milling of hardened steel molds and dies.
Send an Inquiry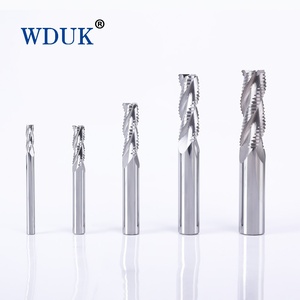
High Precision Wave Flute Roughing End Mill for Aluminum Alloy CNC Machining
Ultra-smooth wave profile ground to prevent material welding and chatter during high-feed milling in non-ferrous alloys.
Send an InquiryMastering Complex Flute Geometry: The Science of High-Gain Cutting Tools
In modern high-speed CNC machining, the structural integrity and surface micro-finish of a cutting tool’s flutes directly dictate tool life, chatter resistance, and surface roughness of the workpiece.
Variable Helix & Asymmetric Pitch
Standard uniform flutes often create harmonics that lead to vibration and poor tool life. Our advanced 5-axis CNC grinding process manufactures end mills with variable helix angles (35°/38°) and unequal indexing, suppressing chatter during deep radial cuts in tough alloys like Inconel and Titanium.
Mirror-Finish Flute Polishing
Micro-grooves left by coarse grinding wheels increase friction and encourage edge buildup (BUE). Utilizing ultra-fine grain diamond and CBN wheels, our factory achieves flute core surface roughness down to Ra < 0.1 µm, ensuring seamless chip evacuation even in sticky aluminum alloys.
Optimized Core Thickness & Gash Geometry
Balancing chip space against tool strength is critical. Our proprietary gash grinding routines reinforce the web thickness of 4-flute end mills while maintaining ample chip clearance, offering up to 40% higher torsional rigidity under heavy feed conditions.
Empowering Ho Chi Minh City’s Precision Manufacturing Hubs
Southern Vietnam has fast evolved into Southeast Asia's powerhouse for electronics, automotive components, plastic injection molds, and high-precision medical device manufacturing. Our custom flute grinding services directly serve factories across Greater HCMC.
Precision Electronics & Micro-Milling Tools
High-tech electronics OEMs require micro end mills with shank diameters as small as 0.2mm for PCB milling and semi-conductor mold manufacturing. Our flute grinding operations ensure exact concentricity (runout < 0.002mm) needed for ultra-fine high-speed spindle operations exceeding 40,000 RPM.
Hardened Steel Tooling for Mold & Die Sector
Factories producing plastic injection molds and die-casting dies require custom 2-flute and 4-flute ball nose end mills capable of machining NAK80, H13, and SKD11 steels (52–62 HRC). We provide customized radius corner fluting that reduces corner wear during complex 3D surface machining.
Automotive Parts & Heavy Metal Deburring Burrs
Suppliers to major automotive and motorcycle OEMs in HCMC depend on our tungsten carbide rotary burrs with single and double-cut flute profiles. Optimized flute depth ensures fast stock removal, minimal vibration, and extended tool life on structural aluminum and cast iron housings.
High-Volume Component Milling & Re-Grinding OEM Solutions
Contract machine shops running 24/7 production lines benefit from our standardized volume production of wave-flute roughing end mills and direct factory regrinding programs, significantly slashing consumable tooling costs per component.
Key Trends Shaping Vietnam’s CNC Tooling & Grinding Landscape
Understanding user intent and market shifts: How Ho Chi Minh City’s machine shops are upgrading tooling strategies to compete globally.
1. Shift toward Custom OEM Tooling
Vietnamese manufacturers are moving away from standard off-the-shelf end mills toward custom-tailored flute geometries. By matching rake angle, helix pitch, and land relief to specific work materials, machine shops achieve 30% faster cycle times.
2. Widespread Adoption of Nano Coatings
Humidity and tough cutting fluids in Southeast Asian facilities demand robust tool protection. Modern flute grinding is now seamlessly combined with PVD coatings such as AlTiN, TiSiN, and DLC (Diamond-Like Carbon) to maintain sharp cutting edges under dry-milling conditions.
3. Rigorous Quality & Traceability Mandates
Supply chain integration requires 100% optical verification. International buyers sourcing from HCMC demand complete batch traceability, geometry inspection certificates, and sub-micron laser measurements for every tool delivery.
Why Leading HCMC Factories Trust Our Flute Grinding Facilities
Combining world-class contract manufacturing processes, certified quality management systems, and specialized engineering support to deliver consistent precision tool grinding solutions.
ISO 13485 & ISO 9001 Certified Quality
Built upon strict quality management protocols utilized in medical and aerospace contract manufacturing. Every grinding wheel dressing, axis calibration, and flute profile is strictly validated under audit-ready standards.
Advanced 5-Axis CNC Equipment Fleet
Our production floor features top-tier CNC tool grinders equipped with multi-wheel packs, in-process probing, and automatic loading robotics, allowing for batch-to-batch repeatability within micro-level specs.
Rapid Prototype to Full Production
Our engineering team provides comprehensive Design-for-Manufacturability (DFM) reviews, building sample tools and testing flute performance before scaling to high-volume manufacturing with fast delivery to Cat Lai Port.
Ho Chi Minh City Buyer Procurement Guide
Essential information for purchasing managers, tooling engineers, and machine shop owners sourcing high-precision flute grinding services and custom end mills.
What specific types of tools can your flute grinding service produce?
Our factory specializes in high-precision grinding of 2-flute, 3-flute, 4-flute, and multi-flute solid carbide end mills, wave-flute roughing cutters, ball nose end mills, thread mills, step drills, surgical drill points, and single/double-cut tungsten carbide rotary burrs. We also engineer custom tools based on step-file drawings.
How do you handle shipping, customs clearance, and delivery to Ho Chi Minh City?
We provide full export management serving major industrial ports in Southern Vietnam, including Cat Lai Port, Tan Cang Hi-Tech Park Port, and Tan Son Nhat International Airport (SGN) for express air shipments. We offer DDP (Delivered Duty Paid) or FOB shipping options, taking care of all customs documentation, Form E CO (Certificate of Origin), and local logistics.
What flute tolerances and surface finishes can your facility guarantee?
We consistently hold flute profile tolerances within ±0.002 mm (2 microns) and radial runout under 0.003 mm. Using fine-grit 1V1 CBN and diamond grinding wheels, flute core surface roughness is finished down to Ra < 0.1 µm, drastically reducing friction and chip welding during high-feed milling operations.
Can you supply specialized PVD coatings suitable for Vietnam's climate and machining conditions?
Yes. We provide a full suite of state-of-the-art PVD coatings applied right after flute grinding, including AlTiN (for general high-temp alloy steel milling), TiSiN (for extreme hardness up to 65 HRC), DLC (for non-ferrous aluminum and acrylics), and CrN (for copper and brass machining).
What is your Minimum Order Quantity (MOQ) and standard lead time for custom tools?
For standardized carbide end mills and rotary burrs, our MOQ starts at 50 pieces per specification. For specialized custom-engineered flute designs, initial prototype batches can be made from 10–20 pieces. Standard production lead times range from 10 to 18 business days, with rush air-freight options available for urgent machine shop downtime situations.
How can our engineering team request a DFM review or quotation?
Simply click the "Send an Inquiry" button on our page to open our direct communication channel. You can submit your 2D/3D tool CAD models (STEP, IGES, DXF), material specifications, and target volumes. An application engineer will evaluate manufacturability and respond with a technical proposal and quotation within 24 hours.
Ready to Optimize Tool Life & Cutting Performance in HCMC?
Partner with a certified factory direct supplier specializing in precision flute grinding, variable helix geometry, and superabrasive CBN tooling solutions.